A battery material recycling line technology converts spent packs into a black mass and a set of metal fractions, and the choice of that technology fixes the energy, the labour and the maintenance that the owner pays every year. You, as a recycling company manager or as a project investor, examine the battery material recycling line technology against the ten-year operating budget instead of the purchase price alone. The cheaper configuration often carries a higher unit cost after the second year.
Which cost items dominate a battery recycling line over time?
The electricity of the shredder and the pumps, the labour of the sorting shift, the replacement of the blades and the treatment of the electrolyte residue form the recurring cost of the plant. A long-term operating cost of battery material recycling review compares a mechanical route with a combined mechanical and hydrometallurgical route, because the second one consumes reagents but recovers a larger share of the metal. You measure the cost for each tonne of product rather than for each tonne of input, and that ratio reveals the real difference. The operating cost then follows the product value instead of the tonnage alone.
How does the technology reduce the labour per tonne?
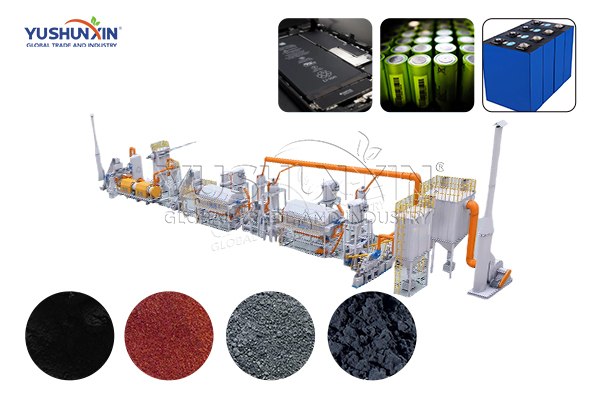
An automated feeding system and a continuous separation circuit remove the manual handling that dominates the labour cost of a small line. A modular battery material recovery line places the controls of several units in one room, and that arrangement allows one operator to supervise the whole process. You train the shift team on the interlock sequence, because a stop caused by a wrong start-up costs more than the training. The plant then runs with a smaller crew and a stable output.
How does the process protect the wear parts?
The discharge of the packs before shredding removes the residual energy that damages the blades, and that step extends the life of the most expensive consumable. A technology that lowers battery recycling operating cost also controls the moisture of the feed, because a wet load accelerates the corrosion of the conveyor and the screen. You record the operating hours of each unit and replace the parts on a schedule, since a planned stop costs less than a failure during a delivery. The maintenance plan then becomes a line in the budget instead of an emergency.
How does the plant verify the saving it achieves?
A monthly report with the energy per tonne, the labour per tonne and the maintenance per tonne shows whether the technology delivers the promised cost. You compare the three indicators with the values of the commissioning test, and that comparison detects a drift before the annual result changes. The plant that publishes the indicators to its own team corrects a small deviation early. The owner then negotiates the next contract with measured data.
Conclusion for recycling companies and project investors
Battery material recycling technology reduces long-term cost through automation, wear protection and a recovery route that captures more of the valuable metal, and those three effects compound over the life of the plant. A battery recycling operating cost advisors team that supplies the mass balance, the maintenance plan and the training programme helps the owner protect the margin. The supply of spent batteries keeps growing, and a line with a low unit cost serves that supply profitably when the metal price moves. If your team needs a reference for the process route and the operating scope, you can learn more about https://www.sxlbp.com/technology/hydrometallurgical-lithium-battery-recycling-plant/ before the next budget review.